Coupled Microstructural Porosity Loss and Anode Overhang Diffusion Kinetics in Aged Prismatic Cells
Coupled microstructural porosity loss and overhang diffusion distort incoming cell capacity tests, requiring standardized multi-day stabilization protocols.
Overhang
Incoming inspection of heavy commercial prismatic lithium-ion cells frequently misidentifies long-term capacity recovery as anomalous cell-to-cell variance. Anode overhang dimensions in high-capacity prismatic formats range between 1.0 and 3.5 millimeters beyond the cathode boundary along the length and height of the wound or stacked jelly roll. This unbacked graphite area acts as an electrochemically active reservoir for cyclable lithium.
During periods of extended dwell at elevated open-circuit voltage, lithium ions migrate laterally from the active electrode area into the overhang region, depressing measurable discharge capacity. Conversely, extended storage at low states of charge reverses this lateral concentration gradient, driving stored lithium back into the working active volume. The resulting capacity fluctuations disguise underlying irreversible inventory degradation, confounding baseline acceptance testing at port entry.
Lateral diffusion kinetics within the graphite overhang operate on time scales spanning hundreds to thousands of hours. The effective chemical diffusion coefficient of lithium within standard synthetic graphite flakes ranges between 10 to the power of minus ten and 10 to the power of minus twelve square centimeters per second. Fickian diffusion across a two-millimeter passive boundary layer requires prolonged resting intervals to attain chemical equilibrium.
Cell screening routines relying on twenty-four-hour rest periods capture transient non-equilibrium states. When procurement protocols fail to account for the spatial redistributions of overhang lithium, early warranty returns trigger unwarranted dispute procedures with cell suppliers over nominal capacity compliance.
A two-millimeter passive overhang introduces reversible capacity shifts up to four percent depending on storage history and rest intervals.
The mechanical stability of large-format prismatic casings influences this concentration exchange. Modern prismatic cells employ rigid aluminum enclosures with external wall thicknesses from 0.8 to 1.2 millimeters. Constrained swelling forces generated during continuous cycling compress the internal jelly roll against the rigid outer walls.
Porosity across the electrode face drops unevenly under mechanical load. Near the outer radii and boundary edges where the anode overhang transitions away from active counter-electrode coverage, mechanical pressure drops sharply. This pressure differential establishes localized variations in liquid electrolyte saturation, altering ionic transport paths into the passive overhang volume.
Factory quality agreements lacking explicit resting condition definitions expose cell buyers to substantial commercial variance.
A typical qualification batch demonstrates the practical impact of this spatial lithium redistribution. Table 1 compiles baseline measurements recorded across five hundred production units assessed under varying rest schedules following ocean transport under standard state-of-charge windows.
| Rest Interval (Hours) | Mean Capacity (Ah) | Standard Deviation (Ah) | Overhang Charge State (%) | Voltage Drift (mV) |
|---|---|---|---|---|
| 24 | 276.4 | 2.8 | 41.2 | 1.4 |
| 72 | 278.1 | 2.1 | 46.8 | 3.8 |
| 168 | 280.5 | 1.4 | 52.3 | 6.2 |
| 336 | 282.2 | 0.9 | 58.7 | 8.5 |
| 720 | 283.4 | 0.6 | 63.1 | 10.1 |
The tabulated figures reveal how incomplete passive diffusion distorts factory verification data. Cells tested at twenty-four hours show depressed capacity values and elevated variance. Extending the thermal equilibration and stabilization window allows overhang equalization, lifting measured capacities above rated thresholds while compressing the lot distribution.
When a supply contract stipulates rejection thresholds within one percent of nominal rating, failure to standardize pre-test rest schedules triggers false shipment rejections at the port of entry.
Tortuosity
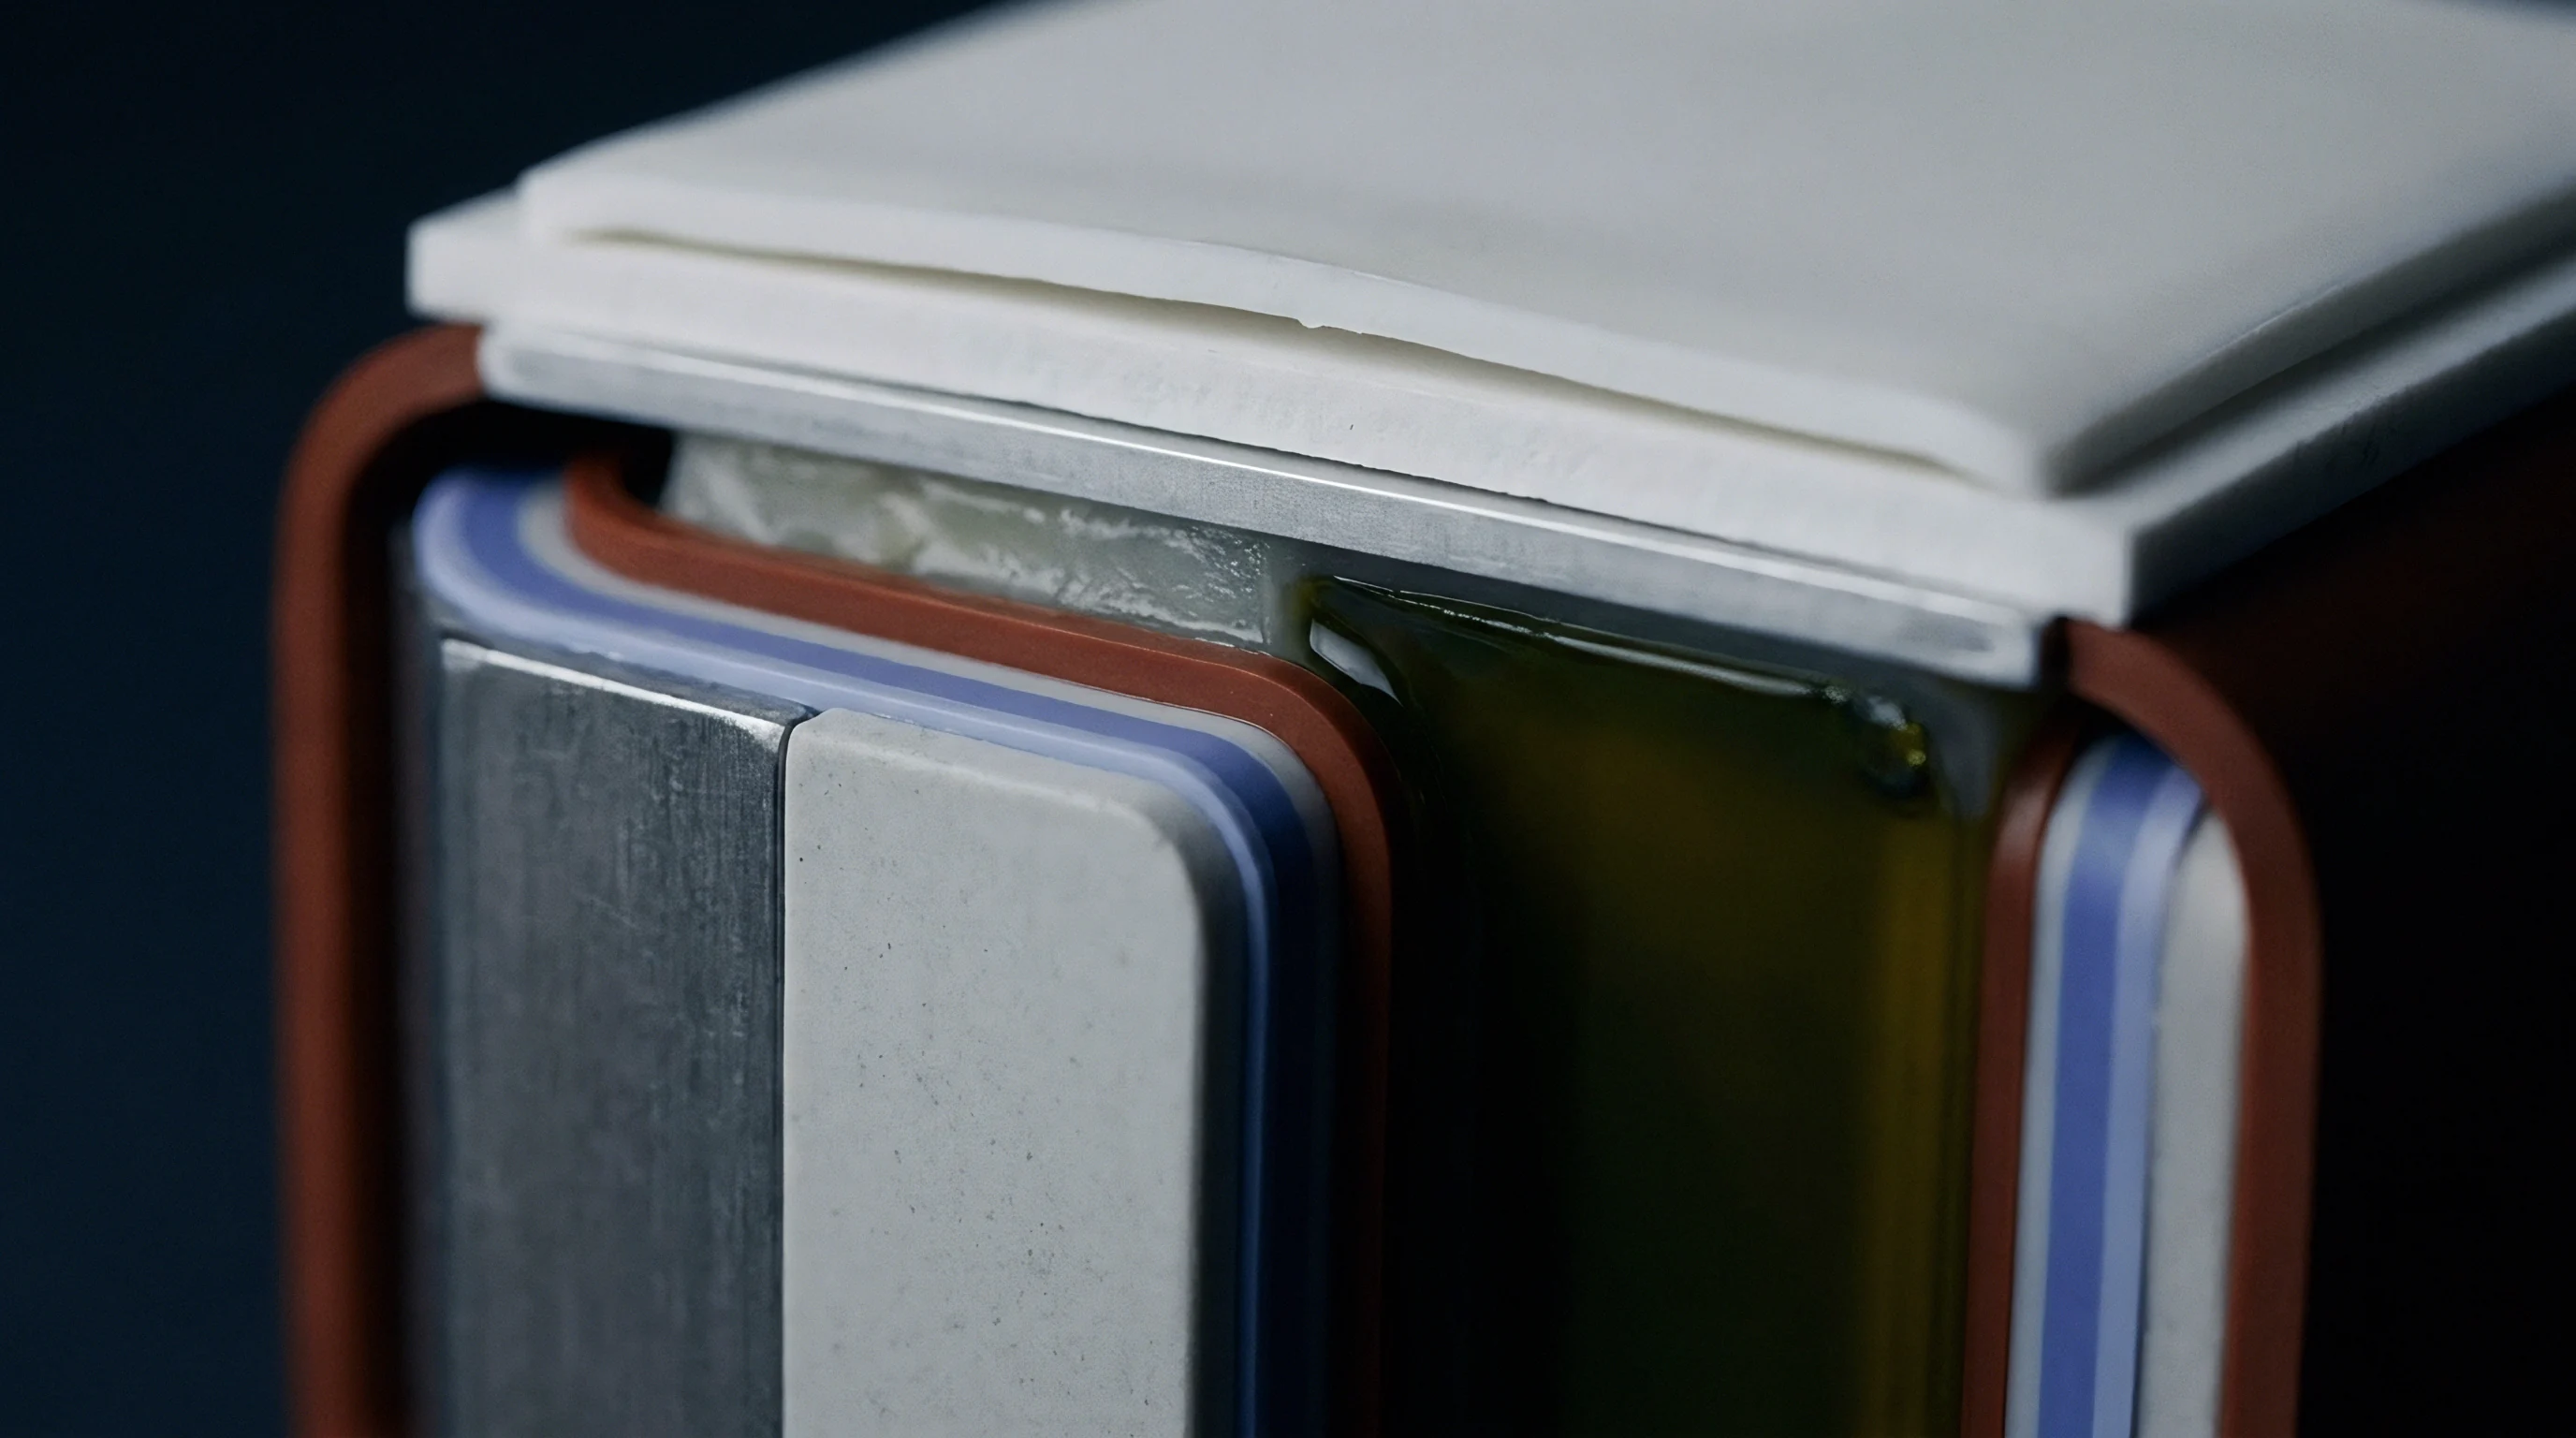
Electrode manufacturing processes establish an initial porous network through slot-die coating and subsequent calendering. Target initial porosity for prismatic graphite anodes settles within twenty-six to thirty-two percent. Calendering increases volumetric energy density while aligning graphite platelets parallel to the current collector foil.
This anisotropic particle alignment increases the directional tortuosity factor perpendicular to the current collector, suppressing through-plane lithium-ion transport. During standard cycling, solid electrolyte interphase development consumes available pore volume, altering effective transport coefficients inside the porous structure.
The MacMullin number characterizes the ionic conduction resistance inside a liquid-filled porous electrode relative to pure bulk electrolyte. This dimensionless quantity links bulk porosity, particle shape factors, and transport tortuosity through established empirical relationships:
- Effective Ionic Conductivity scales inversely with the Bruggeman tortuosity exponent, dropping rapidly once pore volume falls below twenty percent under continuous mechanical restraint.
- Pore Throat Constriction traps liquid electrolyte within dead-end channels, starving active graphite particles of solvated lithium ions during continuous discharge pulses.
- Polymeric Binder Swelling consumes microscopic void spaces near the copper foil interface, driving localized current density spikes toward the electrode surface.
- Interfacial Layer Accumulation compounds cross-sectional narrowing within separator pores and graphite interstitial regions, shifting cell internal impedance upward over operating life.
Over extended operating lifespans, cyclic volumetric expansion and contraction of active graphite particles break the original conductive matrix. Freshly exposed carbon surfaces consume active electrolyte solvents and cyclable lithium ions to form secondary degradation compounds. These reaction products precipitate inside the micro-pores of the negative electrode coating.
Microstructural analysis indicates that a ten percent loss in bulk porosity frequently yields a threefold increase in transport tortuosity, severely constraining liquid-phase diffusion over the entire coating depth.
Calendering density limits fixed during manufacturing define end-of-life fast-charge acceptance boundaries.
The drop in effective transport parameters creates steep lithium-ion concentration gradients across the electrode thickness during charge. Under high charging currents, salt depletion occurs within the deep electrode layers adjacent to the copper current collector. Reaction distributions shift toward the separator interface.
Once the liquid-phase electrolyte potential drops below zero volts versus metallic lithium, metallic deposition initiates on the graphite surface, accelerating capacity fade and increasing thermal runway risks during subsequent field operations.
Boundary
Microstructural degradation across the active-passive border creates sharp discontinuities in local current density. Active graphite regions experience alternating cycles of lithiation and delithiation, driving cyclic lattice expansion up to ten percent along the crystallographic c-axis. The passive overhang undergoes no direct electrochemical cycling, maintaining a relatively static structural lattice.
This physical boundary generates high shear stresses across the graphite coating, causing localized micro-delamination from the copper substrate at the electrode perimeter.
Which Mechanisms Accelerate Interfacial Degradation?
Stress concentrations along the overhang boundary compromise mechanical integrity. Microscopic cracking alters local electrical resistivity, creating pathways for uneven current concentration during high-power operation. Table 2 compiles microstructural parameters and transport properties evaluated across distinct spatial zones of aged 280Ah prismatic negative electrodes after two thousand full-depth cycles.
| Electrode Zone | Final Porosity (%) | Tortuosity Factor | Tortuosity Exponent | Surface Layer Thickness (nm) |
|---|---|---|---|---|
| Central Active Zone | 18.4 | 4.8 | 1.75 | 48 |
| Active Boundary Edge | 15.1 | 7.2 | 2.10 | 82 |
| Overhang Transition Zone | 22.6 | 3.4 | 1.52 | 31 |
| Passive Overhang Core | 28.5 | 2.3 | 1.38 | 14 |
Data gathered across the electrode face demonstrates distinct spatial degradation signatures. The active boundary edge displays the lowest remaining porosity and the highest tortuosity. Severe pore clogging near the perimeter stems from combined direct lithiation and cross-diffusion flux arriving from the passive reservoir.
When fast charging occurs, this localized zone exhibits the earliest onset of lithium plating, creating dendritic deposits along the outer edges of the jelly roll stack.
Safety compliance standards evaluate cells under strict mechanical and electrical abuse regimens. UN 38.3 test protocols require rigorous thermal, mechanical, and vibration verification before dangerous goods transport authorization is granted. IEC 62133 specifies mandatory external short-circuit, overcharge, and continuous charging parameters for stationary and industrial applications.
When localized boundary plating accumulates over extended cycling, cells that passed initial type-testing qualification frequently fail equivalent abuse audits during second-life assessment or long-term operational surveillance.
Clause 8.3 of IEC 62133 places liability for cell-level safety conformity on the pack assembler regardless of underlying supplier degradation kinetics.
Contractual guarantees on cycle life must isolate irreversible active material loss from dynamic overhang exchange. Standard factory test lines apply fixed discharge cut-off voltages to quantify delivered capacity. If boundary transport kinetics become severely sluggish due to high local tortuosity, lithium stored in the passive overhang fails to release within standard test windows.
The measured capacity appears permanently lost. Technical disputes between cell manufacturers and system integrators originate from this kinetic lag, generating unresolvable claims regarding degradation rates.
Acceptance
Receiving inspection protocols for large shipments of prismatic cells require standardized testing frameworks that account for spatial diffusion phenomena. Rapid grading procedures measuring cell open-circuit voltage and internal alternating-current resistance within two hours of container unloading yield invalid screening data. Temperature variations inside marine shipping containers, coupled with extended voyage durations, alter the internal lithium distribution between active and overhang zones.
Incoming qualification workflows demand precise pre-conditioning sequences to ensure measurements reflect true electrochemical capacity.
- Thermal Stabilization holds whole incoming pallets inside temperature-controlled staging rooms at twenty-five degrees Celsius for a minimum of seventy-two hours prior to unboxing.
- Open Circuit Voltage Screening documents pack-level baseline potentials across every incoming serial number to identify outliers exhibiting anomalous internal self-discharge rates.
- Controlled Reference Cycling applies two consecutive symmetric charge and discharge cycles at a constant rate of 0.2C between manufacturer voltage cut-offs to reset interfacial lithium gradients.
- Extended Stabilization Rest enforces a seven-day rest interval at fifty percent state of charge to allow passive overhang equilibration before final impedance grading.
- Direct Current Resistance Characterization applies a ten-second high-rate pulse to quantify true kinetic impedance without interference from transient concentration polarizations.
Deviations from rigorous receiving procedures introduce substantial financial exposure for battery energy storage integrators. A container holding three thousand commercial prismatic cells represents substantial capital investment. Misidentifying transient overhang depletion as manufacturing defects leads to rejected shipments, costly demurrage penalties at port facilities, and broken project delivery schedules.
Integrating structured resting periods inside receiving inspection plans resolves disputes before legal arbitration begins.
Improper lot rejection based on incomplete stabilization creates immediate commercial friction. Cell vendors consistently defend warranty positions by demonstrating that rejected units recover nominal capacity once subjected to multi-day stabilization protocols. A procurement team operating without clear procedural definitions forfeits its commercial leverage.
Clear technical language within master supply agreements aligns verification protocols across factory gate release and port receiving inspection.
Ledger
Warranty frameworks and supply contracts governing large-format energy storage projects must translate electrochemical kinetics into balance sheet provisions. Standard agreements tie capacity guarantees to fixed equivalent full cycle counts or calendar operating periods. These clauses ignore spatial transport phenomena, treating the cell as a homogeneous electrochemical volume.
When microstructural pore loss accelerates local impedance rises, battery management systems trigger premature low-voltage cut-offs under load, depressing usable pack energy even when total cyclable lithium remains largely intact.
Commercial exposure escalates rapidly when project warranties mandate ninety-five percent system availability over ten operating years. Liquidated damages for capacity shortfall typically scale linearly with unfulfilled megawatt-hour commitments. Table 3 illustrates a sensitivity analysis of landed cost and liability accruals for a 100MWh stationary storage project operating under varying assumptions regarding active-area porosity decay and overhang recovery kinetics.
| Porosity Retention (%) | Overhang Trapping Loss (%) | Usable Capacity Fade (%) | Year 5 Penalty Accrual (USD) | Year 10 Replacement Cost (USD) |
|---|---|---|---|---|
| 85 | 1.2 | 14.8 | 0 | 1,250,000 |
| 78 | 2.4 | 19.5 | 180,000 | 3,850,000 |
| 70 | 3.8 | 25.2 | 620,000 | 7,400,000 |
| 62 | 5.5 | 32.1 | 1,450,000 | 11,200,000 |
The figures illustrate the compounding cost of uncontrolled microstructural collapse. Porosity reductions beyond thirty percent accelerate internal resistance, driving usable capacity fade well beyond nominal supplier degradation models. Penalty accruals begin mid-project, culminating in full module replacement requirements before project amortization concludes.
Procurement specifications must stipulate explicit calendered electrode density thresholds, separator pore stability limits, and anode overhang dimensional tolerances to protect the operating margin.
The vendor excuses capacity shortfalls by claiming operating temperatures exceeded warranty conditions during field operations.