Meaning
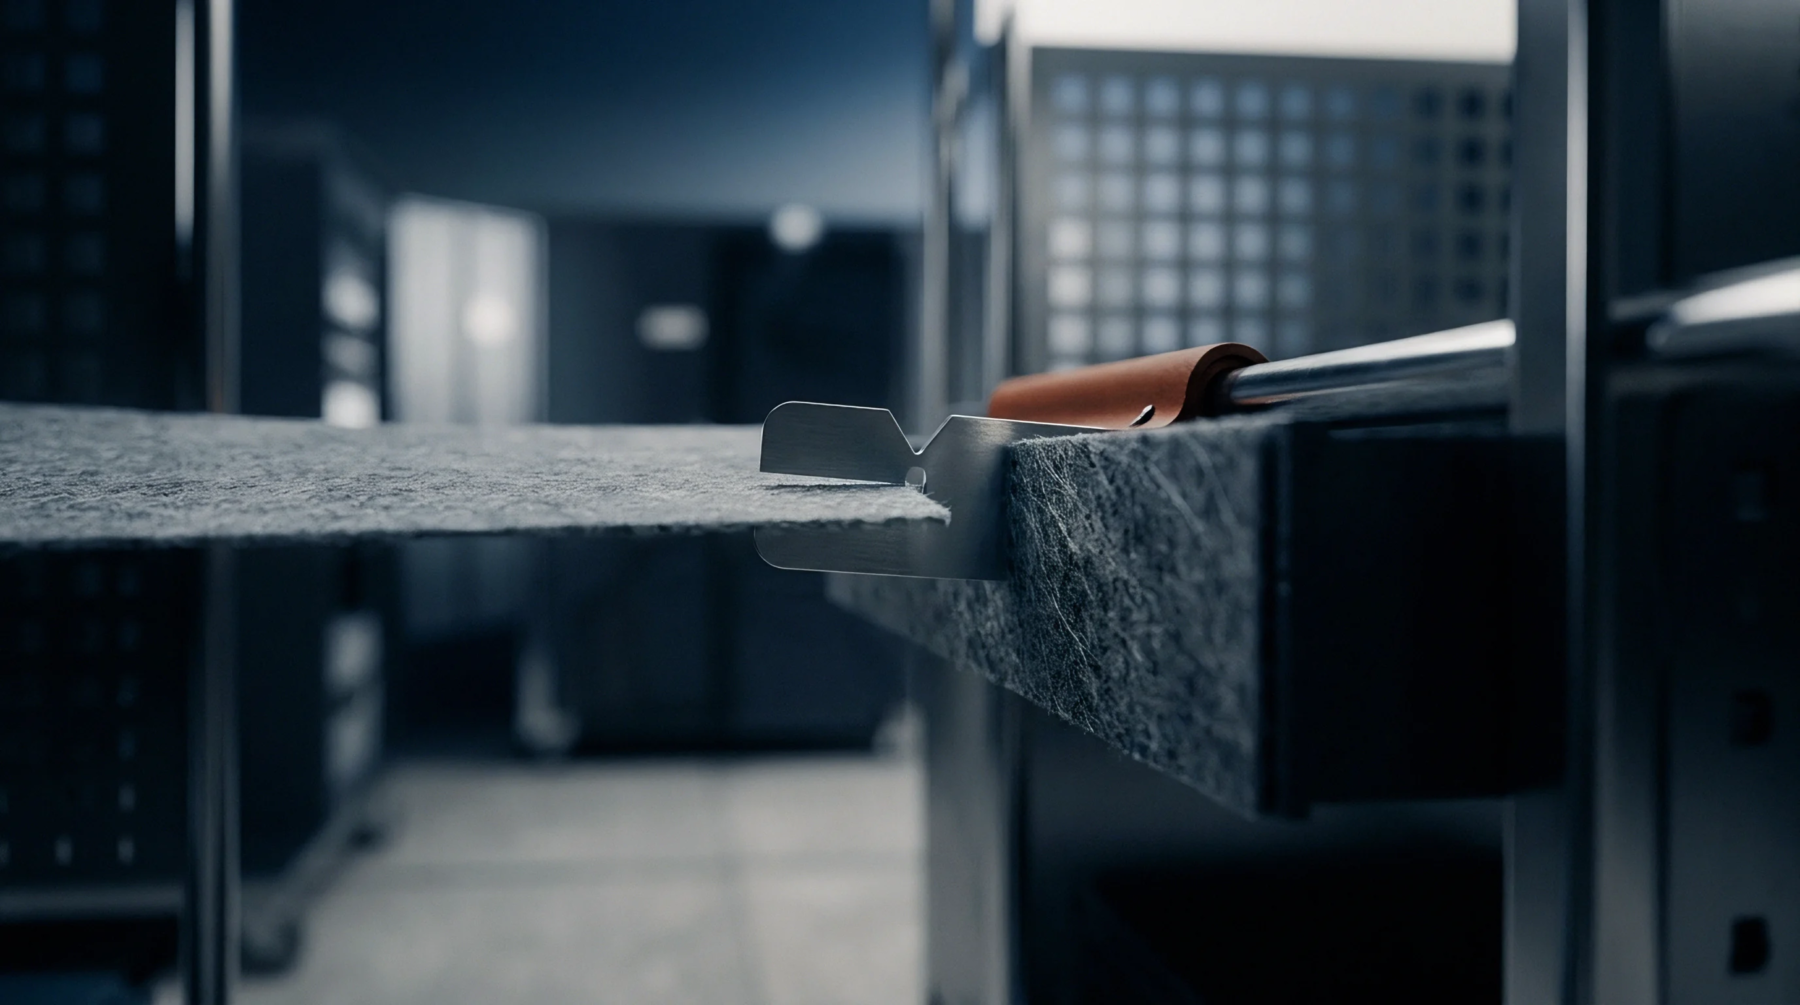
Mechanical separation of wide coated foils into specific widths defines this phase of electrode production. Precise current collector slitting ensures that the active material area aligns perfectly with design specifications for the resulting cell windings or stacks. This process monitors the tension applied to the foil as circular blades divide the copper or aluminium substrate into multiple ribbons.
It governs the edge quality and the total yield of useable electrode material per master roll. The operation reaches its boundary when it encounters unsupported sections where the foil thickness deviates from the standard range. Consistent results here determine the final internal impedance because uniform widths prevent contact resistance variations inside the pack.
Mechanical Process
The machinery utilizes paired rotary knives that create a high precision shear zone. Material enters the nip point under constant tension to maintain straightness during travel. In successful current collector slitting, the blades must penetrate the metal substrate cleanly without generating excessive debris.
Vibration sensors monitor the stability of the slitting hubs to detect early signs of bearing failure. If the alignment shifts by even a few microns, the resulting strips will exhibit wavy edges. These deformations create difficulties during high speed stacking or winding tasks.
Sourcing teams compare slitting speeds to total production uptime to identify the most efficient hardware providers. Reliable hardware maintains alignment throughout long operating cycles without requiring frequent manual interventions. Sharp tool interfaces reduce the energy required to achieve a complete separation.
Material Interaction
The coating layer on the foil creates additional complexity during current collector slitting due to its abrasive nature. Ceramic particles in many formulations accelerate tool wear significantly compared to plain metal processing. High shear forces sometimes cause delamination between the binder and the foil at the cut edge.
This event leaves small zones of bare current collector exposed to the electrolyte. Monitoring the sharpness of the entry point minimizes these mechanical artefacts during normal runtime. Lubrication-free systems are preferred to avoid chemical contamination of the cell interior.
When the thickness of the coating increases, the torque requirements for the slitting drive also rise. Detailed log entries track the linear meters processed before quality drops below acceptable thresholds for edge flatness.
Inspection Standard
Automated vision systems scan the edges to confirm that the slitting results stay within established parameters. These cameras detect missing coating or excessive edge roughness in real time. If current collector slitting produces uneven widths, the resulting capacity of the cell will fluctuate between batches.
Procurement protocols specify the maximum allowed tolerance for these dimensional variations. Deviations often point to wear on the circular knives or errors in the tension control loops. Stable tension prevents the foil from necking down or stretching excessively near the cut site.
Standard operating procedures define when a blade set requires regrinding or disposal to maintain safety. The mechanical precision of the slit edge facilitates reliable long term performance in automotive applications.