Meaning
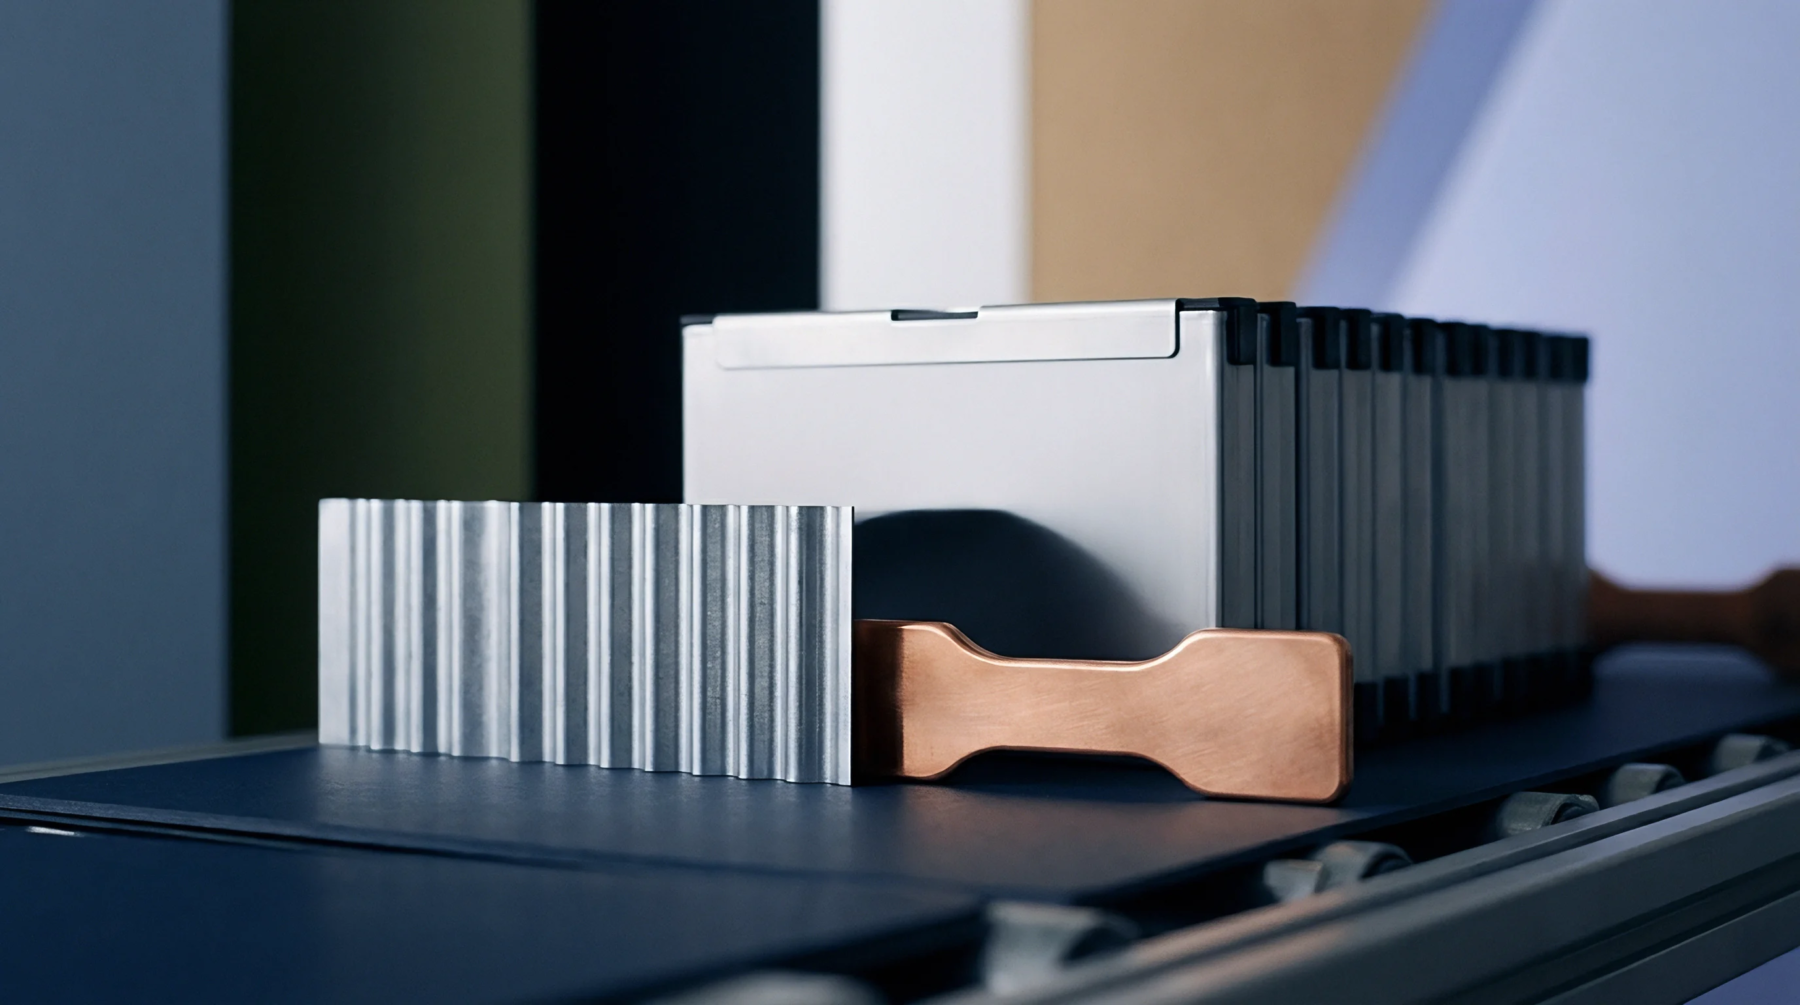
A cylindrical lithium-ion battery format characterized by physical dimensions of forty-six millimetres in diameter and eighty millimetres in height designates this specific energy storage component. Technical standards define 4680 as a tabless architecture designed to reduce internal resistance by removing traditional metallic tabs that connect electrodes to terminals. The geometry allows for higher energy density per unit volume compared to legacy smaller cells while facilitating manufacturing via laser welding.
This unit functions as a building block for battery packs in electric vehicles where the increased size offsets the complexity of interconnecting smaller cylinders. The thermal profile of 4680 changes during high-rate discharge cycles because the shorter path for electrons lowers the heat generated during rapid charging or power output phases.
Structural Performance
Consistent discharge capacity defines the utility of the 4680 across various load requirements in automotive platforms. Energy densities within these cells rely on the chemical composition of the cathode and anode materials rather than the physical casing alone. Manufacturers align the cell chemistry with the 4680 casing to manage the expansion of materials during lithium ion intercalation.
Thermal management systems for these units prioritize the distribution of heat along the wide base of the cylinder to prevent localized hotspots that degrade performance over time. Engineers calibrate the 4680 to survive the vibration and shock loads present in road applications while maintaining internal integrity. Variations in manufacturing precision between batches affect the overall cycle life of the pack.
Proper integration requires matching the power output of the 4680 to the voltage demands of the vehicle architecture.
Manufacturing Efficiency
High speed production lines utilize 4680 to replace assembly methods involving thousands of smaller individual parts. Continuous coating processes deposit active material on electrodes before the machine winds the jelly roll directly into the canister. Laser welding techniques join the collector foils at the base of the 4680 to the current collector plates to create a continuous electrical path.
This automation reduces the time spent on manual handling or complex alignment steps on the factory floor. Operational speed remains a factor in the cost per kilowatt hour achieved during large scale production runs. The simplicity of the internal connections allows for faster throughput than cells that rely on traditional tab welding.
Output quality depends on the maintenance of these welding lasers to ensure every connection remains consistent throughout the life of the battery.
Thermal Management
Effective heat rejection dictates the sustained power output of the 4680 during high current demands. Liquid cooling channels contact the underside of the cells to extract heat efficiently across the wide diameter surface. The architecture of 4680 relies on this bottom cooling to regulate the internal temperature of the jelly roll without relying solely on side wall heat transfer.
Failure to maintain contact between the cell and the thermal plate leads to increased resistance and decreased longevity. Designers specify the contact pressure for the 4680 to ensure thermal transfer remains uniform across all cells in the pack. Proper alignment prevents the development of temperature gradients that might otherwise cause uneven degradation across the module.
The 4680 represents a transition toward large format cylindrical cells to optimize energy density.