Isothermal Electrochemical Swelling Isolation Protocols for Large Format Pouch Cells
Isothermal swelling protocols isolate pure electrochemical lattice expansion from thermal artifacts to deliver precise thickness limits for module engineering.

Kinetics
A large format lithium-ion pouch cell rated above 50 Ah expands along its primary thickness vector through two distinct mechanisms during operation. Reversible swelling tracks the periodic insertion and extraction of lithium ions within the graphite or silicon-graphite anode host lattice during normal charge and discharge cycles. Irreversible swelling accumulates over hundreds of cycles as solid electrolyte interphase growth, electrolyte degradation, transition metal dissolution, and localized gas evolution permanently alter the layer stack.
The anode crystal lattice undergoes unit cell volume variations up to ten percent during full lithiation, driving a macro-level thickness displacement between two percent and five percent across the cell geometry. Uncontrolled temperature spikes mask these electrochemical volume changes through thermal expansion of the aluminum laminate foil, liquid electrolyte, and polymeric separator layers, so isolating thermal from electrochemical effects requires an isothermal boundary during characterization.
Separating these mechanisms requires precise temperature control across the entire planar surface of the pouch. Thermal gradients across large format pouch faces create uneven local current densities, accelerating localized degradation and forming non-uniform swelling pockets. Placing a 100 Ah pouch cell inside an environmental chamber without contact fixtures fails to isolate electrochemical strain because ambient air transfer is too slow to clear the Joule heating generated during 1C or 2C continuous discharge pulses.
As surface temperatures rise, localized thermal expansion obscures the true electrochemical strain profile. Isothermal protocols force direct conduction cooling through high thermal conductivity contact plates, keeping surface temperatures within plus or minus 0.2 degrees Celsius across the active pouch area during heavy current throughput.
Isothermal contact fixtures maintaining surface temperature within 0.2 degrees Celsius isolate pure electrochemical lattice strain from bulk thermal expansion.
Lattice strain measurements under fixed mechanical constraints reveal the true stress response of the cell stack. Restricting a pouch cell from expanding in thickness converts internal intercalative strain directly into normal compressive stress against the bounding plates. The initial mechanical pre-load, typically set between 20 kilopascals and 50 kilopascals, shifts dynamically with the state of charge, peaking at full lithiation near one hundred percent state of charge.
Secondary phase transitions within nickel-rich NMC cathode materials cause non-linear structural contractions at high voltages, producing complex force-displacement hysteresis loops between charge and discharge legs. Quantifying this dynamic force response under isothermal conditions provides the baseline material parameters needed to design pack-level mechanical retention systems.
Gas evolution introduces a distinct volumetric signal that alters the mechanical force profile. Parasitic reactions between non-aqueous carbonate electrolytes and active electrode materials generate trace carbon dioxide, carbon monoxide, ethylene, and hydrogen. Trapped gas forms pockets between electrode leaves, swelling local stack thickness and reducing contact area between active layers.
Without external pressure, these pockets yield inflated volumetric expansion readings that do not correspond with crystallographic lattice strain. Applying a calibrated, uniform pre-load flattens gas pockets toward the perimeter, preserving uniform internal stack impedance while load cells record pure solid-phase swelling forces. Disentangling gas generation rates, solid-phase expansion, and mechanical restraint remains difficult when cell skin temperatures drift by even two degrees Celsius.

Clamp
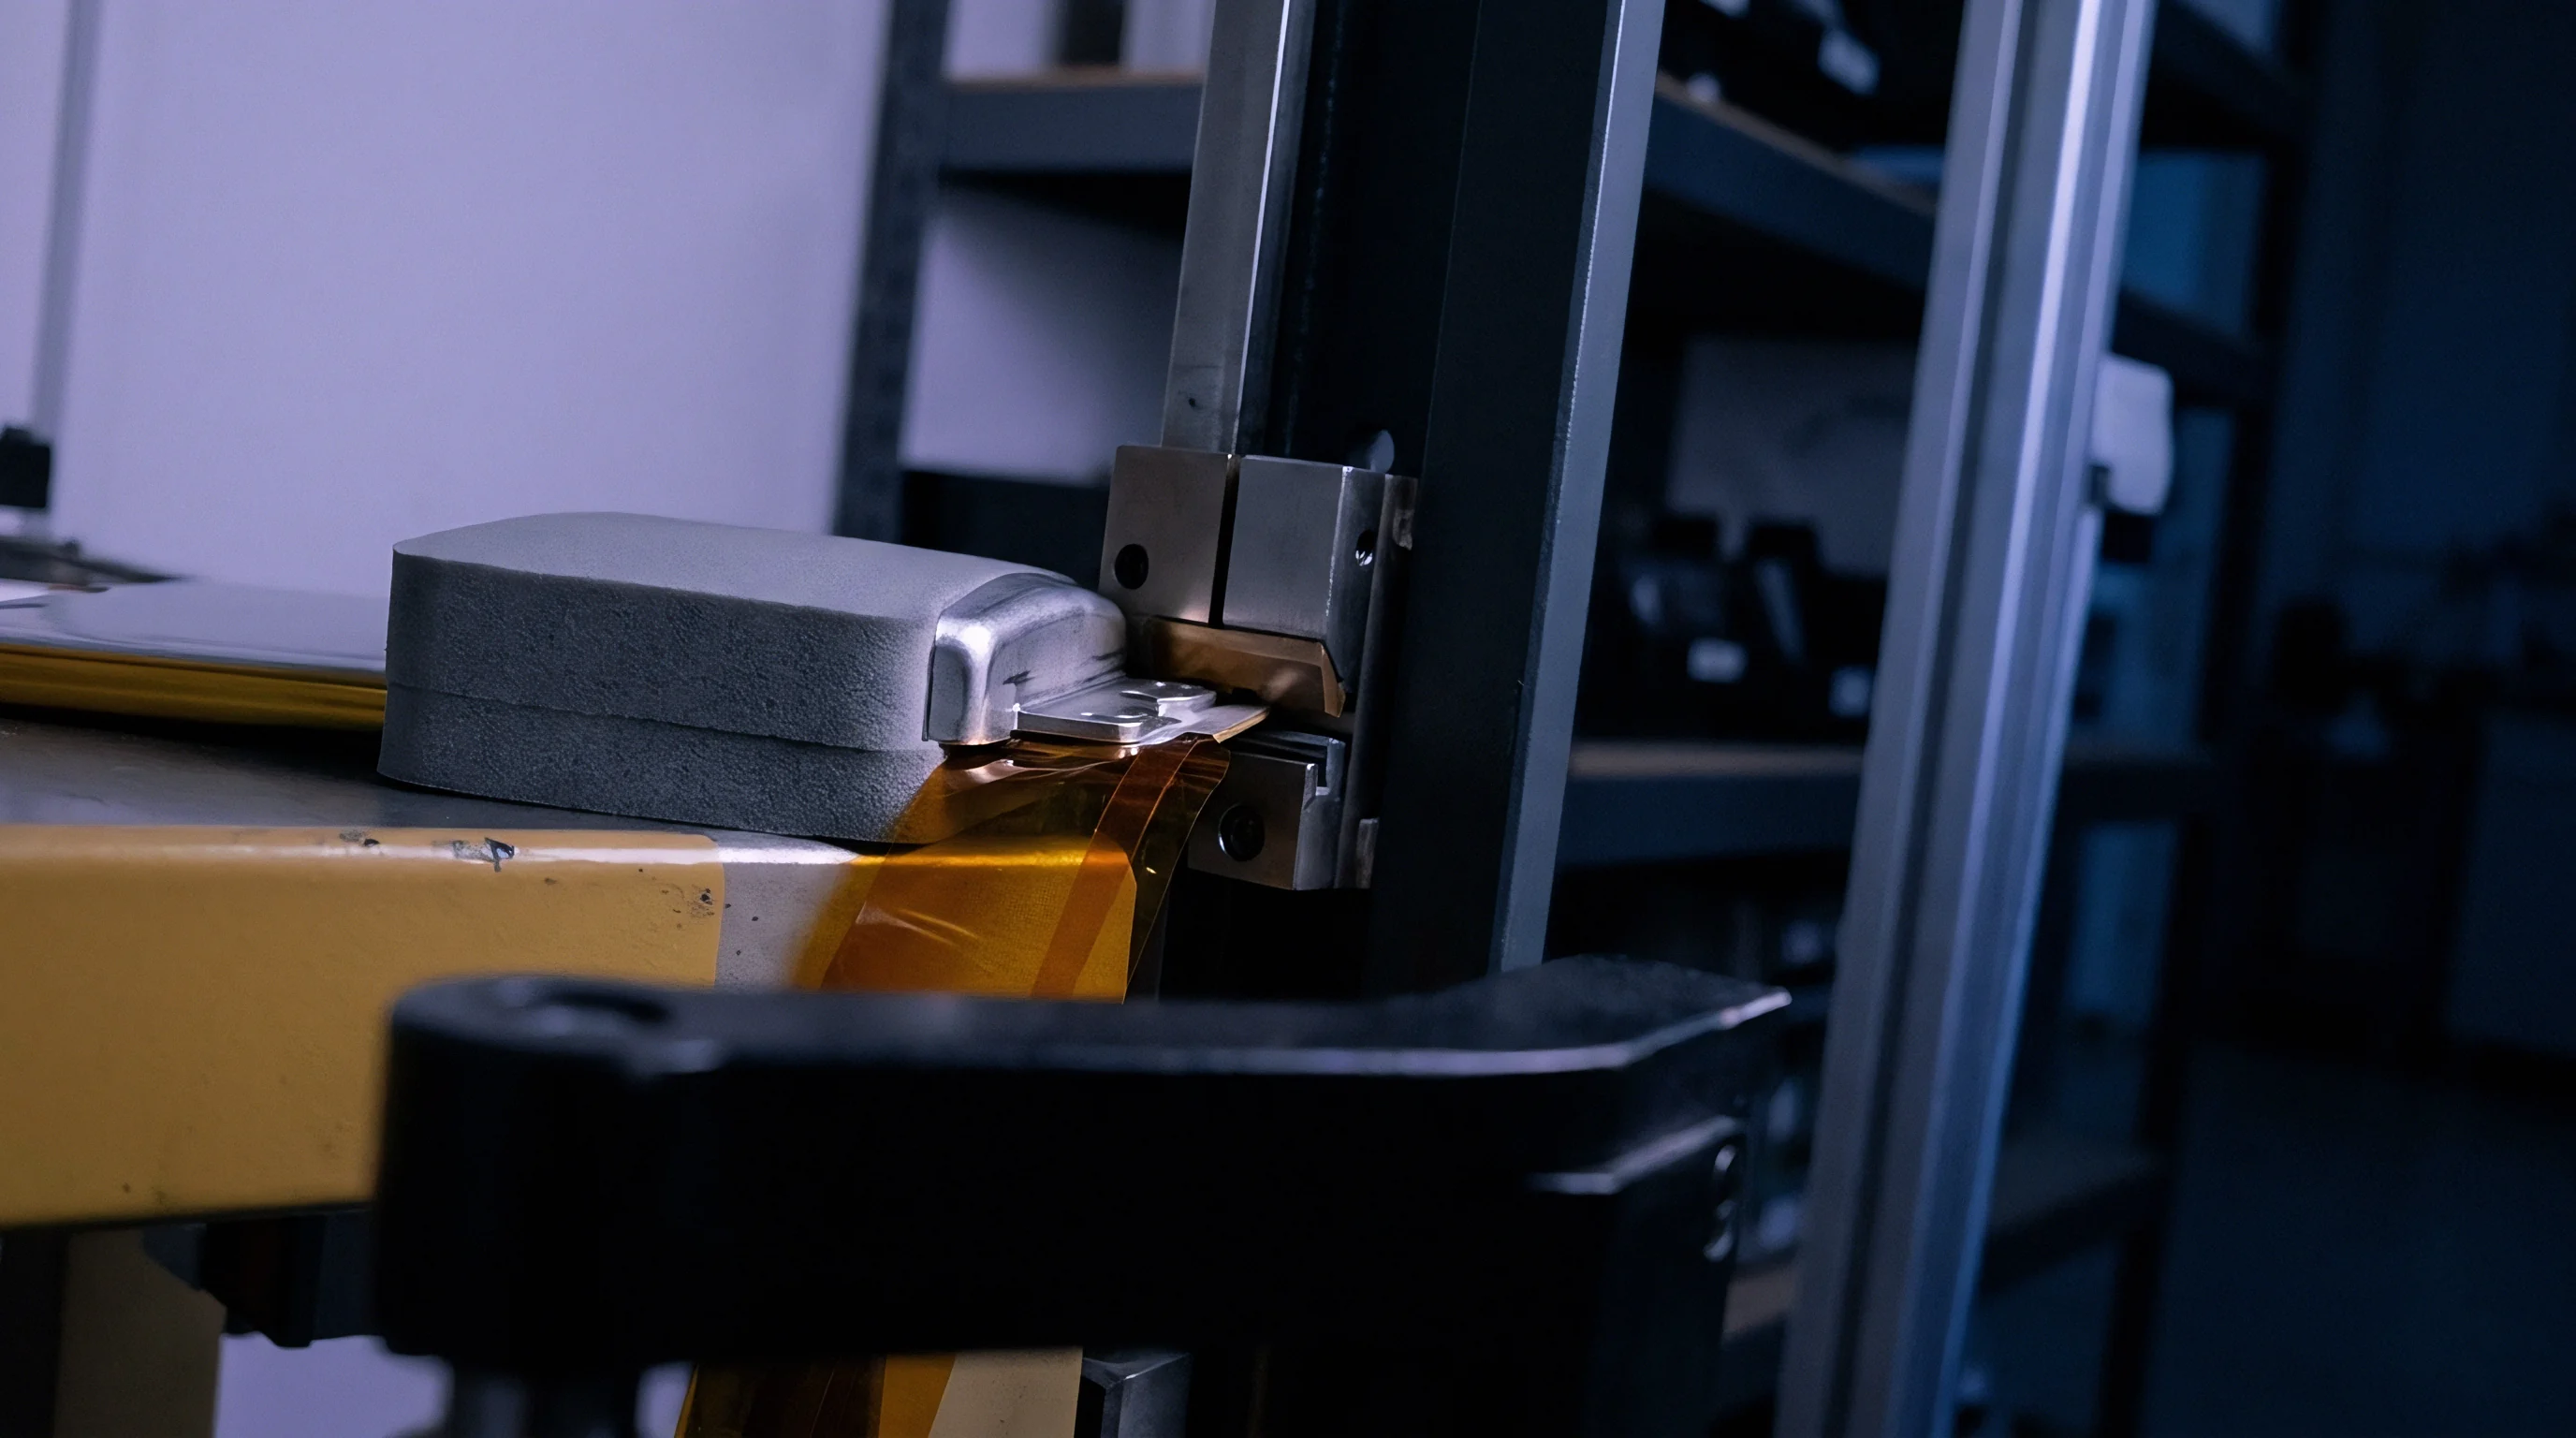
Mechanical isolation fixtures for pouch cell swell characterization rely on rigid aluminum or stainless steel compression plates driven by precision lead screws or hydraulic actuators. Frame rigidity governs measurement accuracy: structural deflection under peak swelling loads dampens the force signal and underreports true internal stress. High-precision test rigs therefore use load frames engineered for axial stiffness exceeding 50 kilonewtons per millimeter.
Integrating load cells with temperature-compensated strain gauges prevents thermal drift from skewing long-term force logs, while placing transducers directly behind the active pressure plates captures normal dynamic force variations without taking on bending moments from asymmetrical cell expansion.
| Fixture Component | Material Parameter | Tolerance Standard | Operational Impact |
|---|---|---|---|
| Compression Plate | Hard-anodized Al 6061-T6 | Flatness within 0.02 mm | Prevents localized pressure spikes across active stack |
| Load Frame Structure | Structural Steel A36 | Stiffness over 50 kN/mm | Eliminates frame deflection during peak state of charge |
| Thermal Interface Layer | Pyrolytic Graphite Sheet | Conductivity over 1000 W/mK | Ensures isothermal heat removal across pouch surface |
| Force Transducer | In-line S-beam Load Cell | Accuracy within 0.05% FS | Captures sub-Newton force variations during breathing |
Thermal regulation within the fixture relies on fluid-circulating cold plates integrated directly into the bounding clamp structure. Internal cooling channels fed by a closed-loop lab chiller maintain high heat transfer coefficients across the active pouch surface. Pyrolytic graphite sheets or silicone-free thermal pads sit between the cold plate face and the outer aluminum laminate skin.
Proper electrical insulation is necessary to prevent high-voltage shorting if the outer pouch foil develops micro-abrasions during assembly or long-term cycling. Silicone-based thermal interface materials are strictly avoided on high-reliability test benches because volatile siloxanes migrate into electrical contacts and optical sensors, triggering contact resistance failures in adjacent instrumentation.
Position sensors measure sub-millimeter displacement changes when cells undergo testing under constant-force control regimes. Linear variable differential transformers or laser displacement sensors achieve spatial resolutions below 0.1 micrometers. Aligning displacement sensors along the central axis of the pouch face avoids edge-curl artifacts around the perimeter seal, where excess laminate and unbonded separator edges expand independently of the active electrode stack.
Isolating the active face measurement zone from the perimeter seal is necessary to generate valid empirical engineering data for pack design.
IEC 62660 testing guidelines mandate constant temperature monitoring across cell terminals to verify thermal equilibrium during high C-rate cycling.
Clamp calibration procedures account for system-level thermal expansion. Heating the metallic plates during temperature-step protocols causes thermal growth in the fixture columns, which displacement sensors register as false cell compression. Running dry calibration runs with non-expanding ceramic calibration blocks across the target temperature range generates baseline correction curves that software algorithms subtract from raw sensor data in real time.
Omitting system calibration introduces errors up to twenty micrometers in displacement metrics, corrupting early-cycle solid phase lattice expansion data.
When fixture stiffness is inadequate, structural frame deflection understates internal stress buildup. Sizing thermal management loops without calculating peak cell Joule heating leads to thermal runaway on the test bench during fast-charge swelling trials. If temperature isolation fails, cell core temperatures spike, triggering accelerated electrolyte oxidation and swelling figures that do not match field data.


Mapping
Decoupling electrochemical strain requires structured matrix sweeps across temperature, charge rate, and state of charge limits. The test matrix begins with standard formation cycling followed by C-rate characterization sweeps ranging from 0.1C to 3.0C at fixed temperatures of 10, 25, and 45 degrees Celsius. Low C-rates minimize active internal Joule heating to establish a clean baseline for crystallographic phase-change swelling, while higher C-rates evaluate dynamic solid-state transport limitations, localized concentration polarization, and lithium plating kinetics.
Active chiller feedback loops hold cell ambient skin temperature constant throughout each leg.
What Loading Pressure Isolates Breathing from Degradation?
Maintaining an initial mechanical pre-load between 30 kilopascals and 50 kilopascals across the pouch surface compresses soft gas pockets and ensures uniform interfacial contact without inducing mechanical creep in the separator. Lower pre-load pressures permit interfacial gapping and localized pouch ballooning. Higher pre-load pressures exceeding 150 kilopascals risk crushing the porous structure of polymeric separators, reducing ionic conductivity and accelerating dendrite nucleation across electrode edges.
The optimal isolation pressure flattens manufacturing variations in cell flatness while recording uncorrupted lattice expansion vectors.
Characterization sequences enforce rigid procedural boundaries to capture reproducible physical metrics.
- Mount the pre-conditioned pouch cell within the isothermal load frame with pyrolytic graphite contact sheets, applying a calibrated 30 kilopascal baseline pre-load.
- Connect closed-loop chiller lines to the cold plates, setting fluid temperature to 25.0 degrees Celsius, and soak the system for two hours until load thermal equilibrium is reached.
- Execute a three-cycle 0.1C charge and discharge reference loop while logging load cell force, displacement, voltage, and current at 10 Hertz sampling rates.
- Perform step-wise 10 percent state of charge holds with one-hour relaxation periods to record fully relaxed open-circuit electrochemical equilibrium swelling values.
- Increase charge rates sequentially up to the maximum rated pulse current, checking for irreversible force offsets that indicate mechanical separator collapse or lithium plating.
Maintaining a static pre-load of 30 kilopascals compresses soft gas bubbles without distorting the internal separator pore structure.
Data processing converts raw force-displacement curves into differential swelling profiles plotted against cell state of charge. The derivative of thickness evolution relative to state of charge highlights major phase transitions within the anode and cathode host materials. In nickel-rich NMC chemistries, distinct peaks in differential swelling correspond to structural phase transitions between hexagonal and monoclinic crystal structures.
Shifts in peak position over extended cycle life reveal loss of active lithium inventory and cathode degradation prior to catastrophic capacity loss on the circuit channel. Continuous monitoring of differential expansion metrics provides a non-destructive analytical tool for tracking internal battery state of health.
| State of Charge (%) | Reversible Swelling (mm) | Constrained Stress (kPa) | Dominant Phase Mechanism |
|---|---|---|---|
| 0 to 20 | 0.02 to 0.05 | 35 to 50 | Dilute stage graphite intercalation |
| 20 to 60 | 0.05 to 0.18 | 50 to 110 | Stage 2L and Stage 2 graphite transitions |
| 60 to 90 | 0.18 to 0.32 | 110 to 180 | Stage 1 graphite lithiation and NMC monoclinic shift |
| 90 to 100 | 0.32 to 0.45 | 180 to 260 | Full C6 lithiation and cathode anisotropic contraction |
Discrepancies in published swelling curves often trace to variations in fixture torque or thermal cooling delays during third-party testing. Standard factory characterization, by contrast, relies on unconstrained optical thickness measurements, which inherently reflect gas generation and thermal expansion alongside lattice changes.

Stack
Translating single-cell isothermal swelling measurements into module and pack structures depends on accurate compression pad design. Large format pouch cells are rarely installed without elastomeric foam pads sandwiched between adjacent cells in a mechanical module. These compression pads serve a dual mechanical role: absorbing reversible cell thickness variations over each charge-discharge cycle and maintaining minimum required interface pressure at end of discharge when the cell shrinks.
Polyurethane, silicone, and microcellular foam materials exhibit non-linear stress-strain relationships that evolve under continuous cyclic compression over operational lifespans.
Selecting pad materials requires balancing long-term compression set resistance against dynamic spring rates. Soft foams with low initial compression modulus yield under light loads, failing to provide adequate pre-load force at low state of charge. Extremely stiff elastomeric foams exert excessive force against module end-plates at full state of charge, leading to structural housing fatigue or fastener shear failures.
The spring rate of the chosen pad must match the cell’s differential swelling profile across the operating temperature window, allowing mechanical engineers to model load-frame interaction using finite element analysis tools.
Improper compression budgeting across the module assembly triggers multiple failure modes inside the pack enclosure.
- Interfacial Delamination occurs when internal mechanical pressure drops below 10 kilopascals at low states of charge, permitting electrode layers to physically separate during vehicle vibration.
- Separator Creep Failure happens when peak expansion forces at high states of charge exceed 300 kilopascals, causing plastic deformation of the separator and localized short circuits.
- Busbar Fatigue Fracture results from excessive cell thickness growth pushing cell terminals outward, inducing cyclic bending stresses on rigid laser-welded interconnects.
- End-Plate Yielding develops when cumulative end-of-life swell forces exceed structural housing yield strength, bowing the pack frame and breaching environmental seals.
Because cold charging triggers lithium plating and accelerates volume expansion, plating events produce sharp, irreversible force increases during charge cycles, creating localized structural stresses that are easy to observe on constrained test rigs. If the module enclosure cannot absorb end-of-life irreversible swelling, internal pressure rises past critical limits, triggering rapid capacity fade and localized lithium plating near current collector tabs.
Selecting compression foam stiffness without mapping end-of-life irreversible swelling leads directly to busbar fatigue failure.
Because foam stiffness governs operational lifetime, designing module mechanical constraints requires balancing cell life retention against structural mass penalties. Applying light mechanical restraint maximizes structural margins while sacrificing cycle life performance.

Provision
Procurement documents for large format pouch cells require clear, enforceable engineering definitions for dimensional tolerances, swelling limits, and testing validation rules. Standard commercial datasheets typically state cell thickness as a single nominal figure at fifty percent state of charge with a loose tolerance of plus or minus 0.5 millimeters. This window is far too broad for high-density pack integration: a stack of twenty cells risks a cumulative tolerance variation of ten millimeters.
Sourcing specifications must state cell thickness as a function of state of charge, temperature, applied pre-load pressure, and cycle age.
Quality assurance clauses define specific test protocols that delivered cell batches must meet during incoming inspection audits. Incorporating detailed isolation protocols into cell specifications resolves potential disputes over non-conforming lots. When inspection reveals thickness variations exceeding drawing limits, disputes frequently center on measurement methods ~ such as load plate flatness, temperature control, or clamp pressure calibration.
Mandating standard isothermal test fixtures and defined clamp protocols within the master supply agreement eliminates ambiguity during quality claims.
Contractual provisions for cell supply agreements mandate comprehensive dimensional characterization dossiers prior to production tooling sign-off.
- Beginning of Life Nominal Thickness measured under a calibrated 30 kilopascal load at 25 degrees Celsius across 0, 50, and 100 percent state of charge states.
- Reversible Swelling Coefficient defined as the maximum thickness change per unit state of charge during a 0.5C charge and discharge cycle.
- End of Life Swelling Threshold setting the maximum allowable irreversible thickness increase at 80 percent state of health retention under continuous cycling.
- Test Isolation Compliance Report providing raw load cell and thermal tracking logs from an independent certified laboratory validating protocol adherence.
When data sheets omit preload, yield drops immediately and the warranty seam shifts back to the integrator if mechanical isolation testing is left out of validation dossiers. Tooling costs scale fast when module end-plates must be re-engineered late in the product launch timeline.
Under Standard Warranty Clause 14.2 of international battery supply agreements, the cell manufacturer assumes liability for cell stack thickness evolution only when the pack integrator demonstrates that mechanical containment forces within the module were maintained between 20 kilopascals and 200 kilopascals throughout the operational life of the asset.