Thermal and Mechanical Stress Degradation Mechanisms in Prismatic Formats
Constraining prismatic cells between 300 and 500 kPa prevents electrode delamination and suppresses localized lithium plating over long cycle life.


Swell
Lattice strain sets off internal structural shifts inside prismatic lithium-ion cells well before any external expansion shows up during incoming inspection. As the cell charges, lithium ions intercalate into the negative electrode host, pushing the graphite lattice out along its crystallographic c-axis by about 10 percent. Adding silicon to boost volumetric energy density magnifies this local expansion, building up sharp hydrostatic pressures inside the cell.
Because the rigid aluminum can ~ typically deep-drawn or welded at 0.6 mm to 1.2 mm thick ~ prevents the narrow edges from expanding, that mechanical stress pushes out against the broad faces, turning microscopic intercalation strain into macro-scale casing deflection.
Without external restraint, prismatic cells flex unevenly across their broad faces. A rectangular metal container holds internal pressure well at its rounded corners, but the flat central area behaves more like a flexible membrane. When gas generates from solid electrolyte interphase breakdown and micro-cracking across active cathode particles, that internal gas pressure compounds the mechanical swelling force.
On continuous fast-charging cycles, unconstrained cells can bulge at the center by more than 5 percent of their nominal casing depth. This expansion squeezes liquid electrolyte out of the high-pressure center and into perimeter voids, drying out the core of the electrode stack.

Lattice Strain and Anode Volumetric Breathing
Phase changes in the active electrode materials dictate how much mechanical workload the enclosure has to absorb. In lithium iron phosphate, intercalation follows a two-phase transition between iron phosphate and lithium iron phosphate, changing unit cell volume by about 6.8 percent. Nickel-rich layered oxide cathodes contract anisotropically along the c-axis at high states of charge, causing intergranular micro-cracks between primary grains.
These fractures expose unpassivated metal surfaces to liquid electrolyte, steadily consuming active lithium through ongoing interphase growth. As reaction byproducts build up inside the porous electrode structure, the solid layer thickens permanently, layering an irreversible swell on top of the reversible breathing from state-of-charge cycling.
Graphite anode breathing drives most of the short-term dimensional changes during cycling. As lithium enters the graphite, stage transitions widen interlayer spacing from 0.335 nm to 0.370 nm when fully lithiated to stage one. In high-density electrodes pressed past 1.6 g/cm³, the microscopic pores simply cannot absorb this volumetric growth.
The solid active grains push hard against neighboring particles and conductive carbon networks, shifting the entire jellyroll or z-folded stack against the interior walls and transferring that mechanical load straight into the external module frame.
Thick aluminum prismatic cans require external mechanical restraint to prevent central face bowing, since internal gas generation and lattice expansion will otherwise turn unconstrained volumetric growth into permanent plastic deformation.
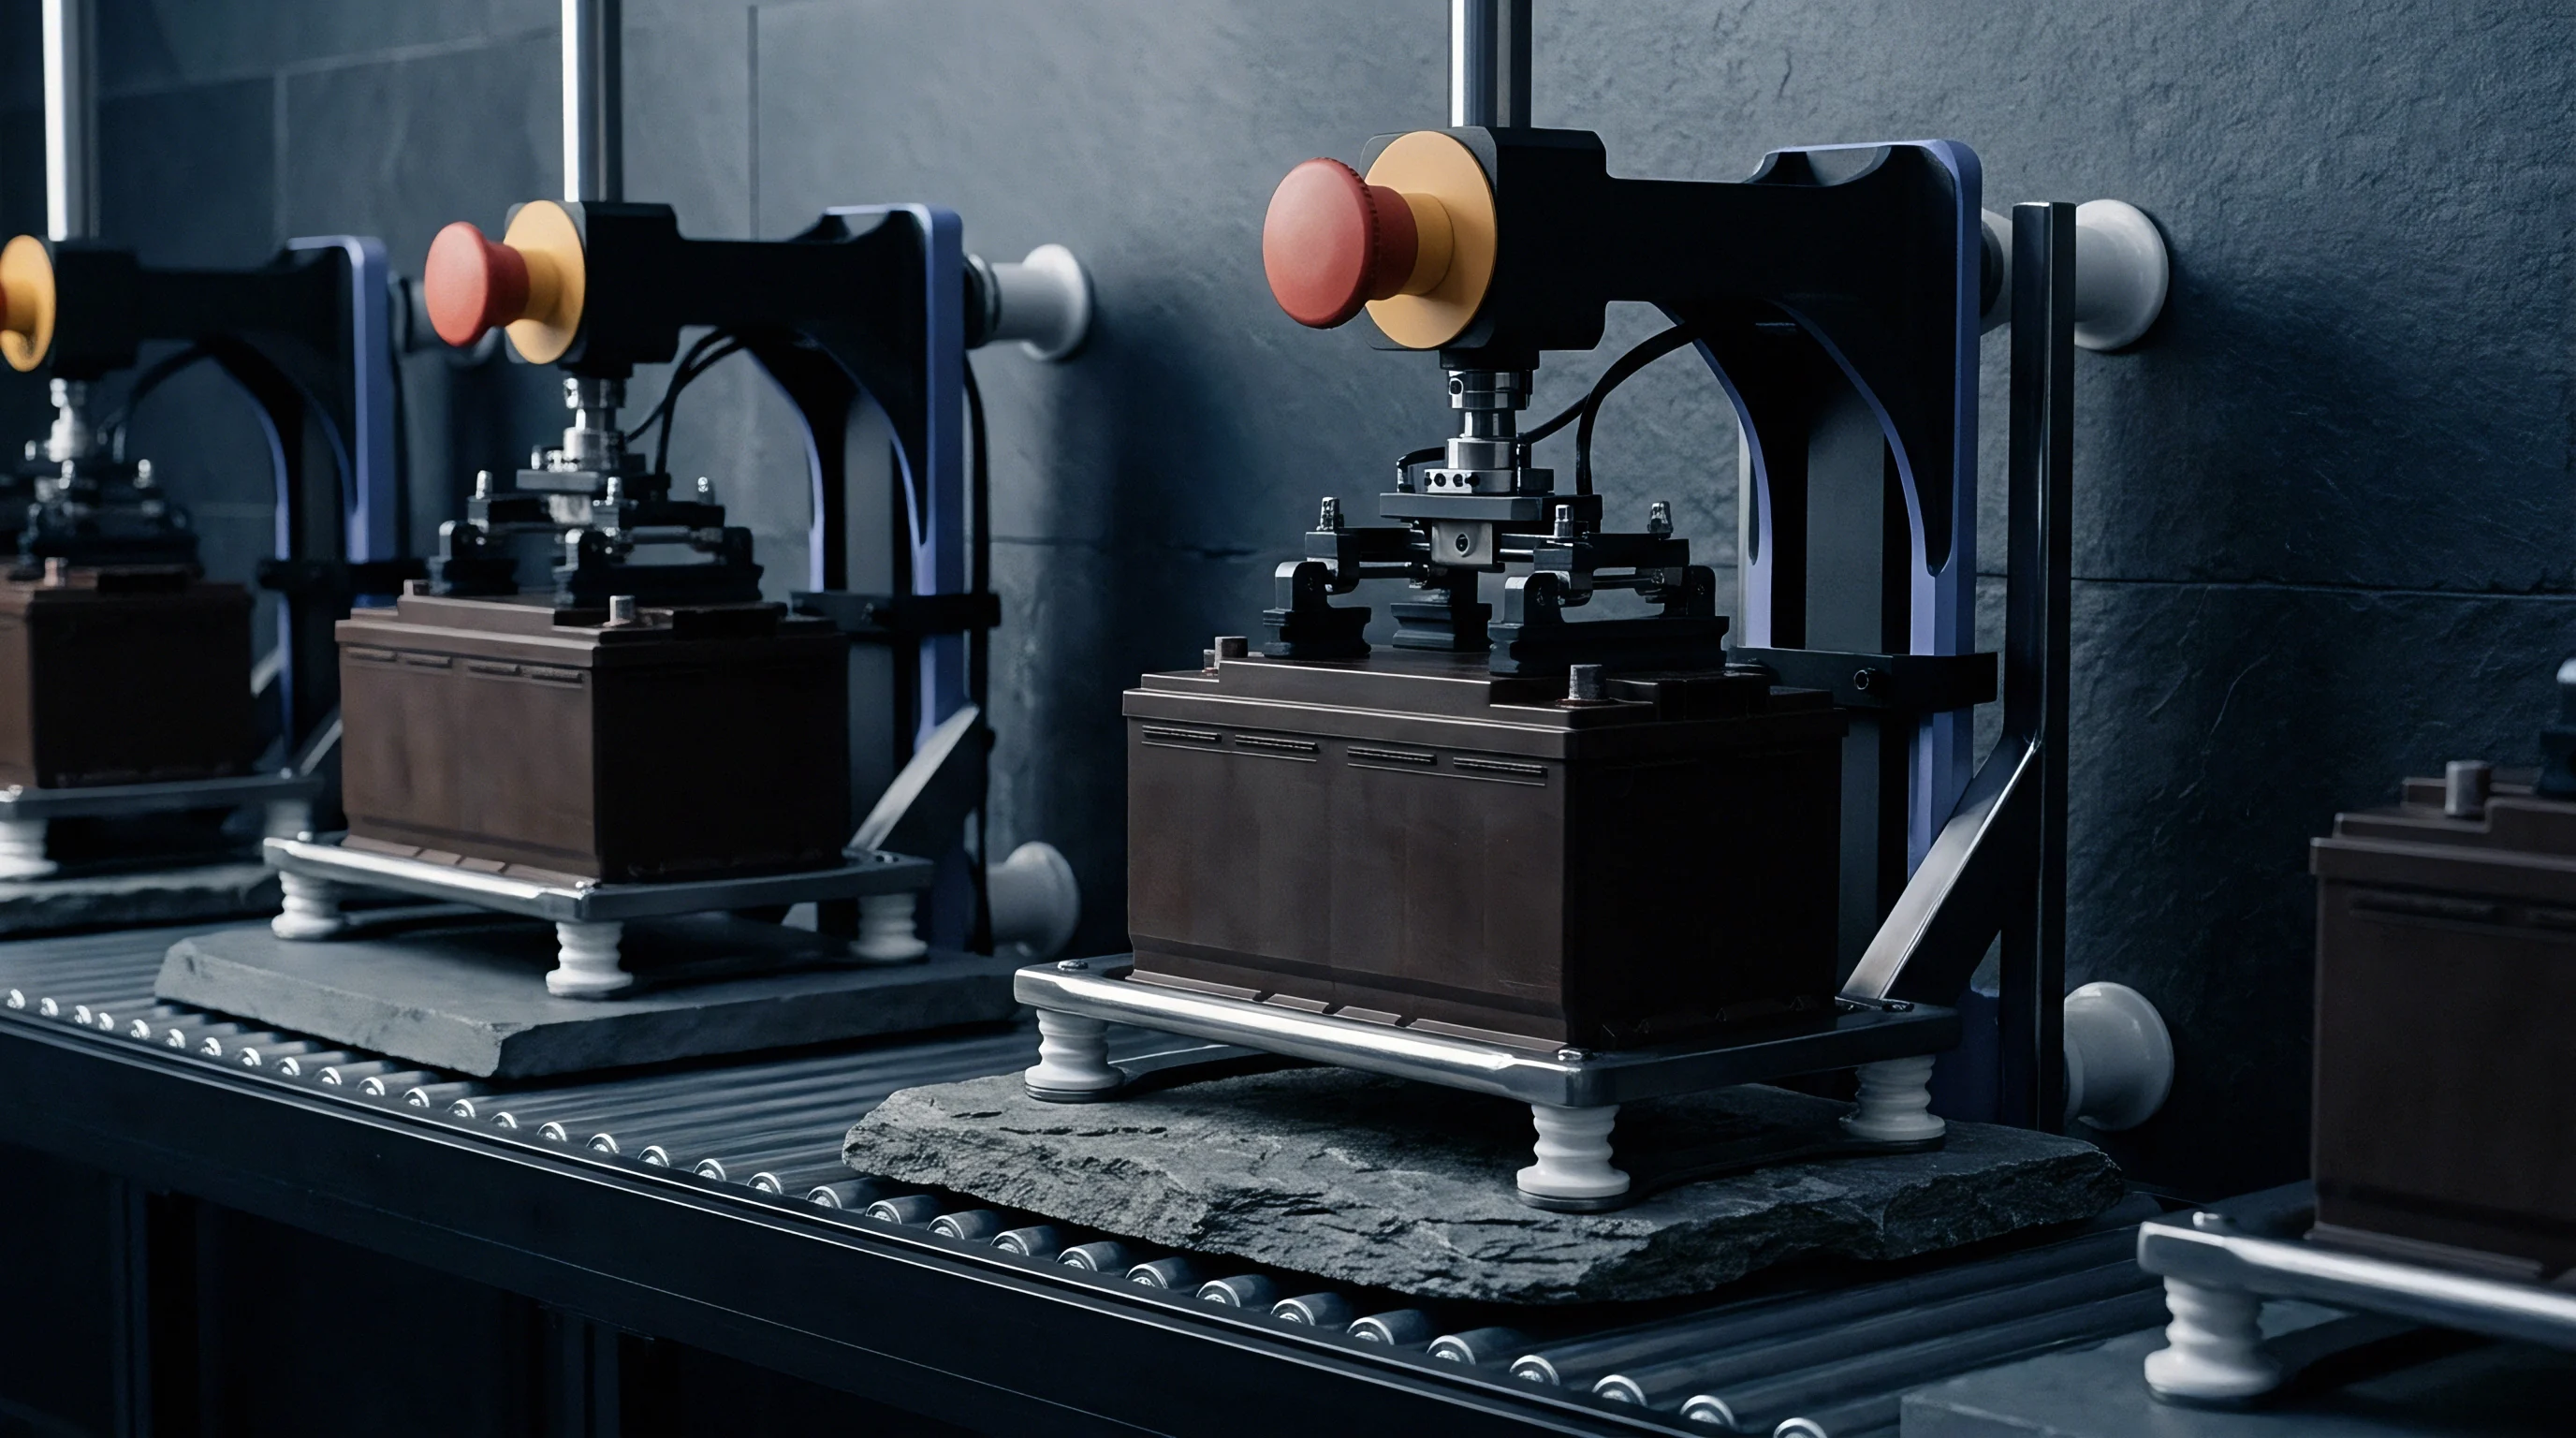
Hard Shell Spatial Constraints and Gas Pressure Evolution
The rigid geometry of an aluminum can forces volumetric material growth to turn into internal compressive stress. Unlike pouch cells, which swell somewhat uniformly across flexible laminate faces, prismatic cans are exceptionally stiff along their welded seams and corner radii. This makes internal pressure across the broad faces far from uniform: peak compressive forces gather near the center, while pressure tapers off toward the outer edges.
Gas accumulation inside sealed prismatic housings adds another layer of mechanical stress. Electrolyte reduction generates volatile hydrocarbons, carbon dioxide, and hydrogen during high-temperature storage or aggressive high-voltage operation. Before the safety vent opens ~ typically set between 0.4 MPa and 0.8 MPa ~ this gas builds internal static pressure inside the rigid can.
That pressure exerts continuous tension on the welded top cover and bottom header plates, straining perimeter seams and risking micro-fissures along the laser weld tracks.
| Chemistry Architecture | Graphite Anode Expansion (%) | Cathode Lattice Shift (%) | Irreversible EOL Swell (%) | Peak Core Stress Unconstrained (MPa) |
|---|---|---|---|---|
| LFP / Synthetic Graphite | 9.2 | -6.8 | 3.5 – 5.0 | 1.2 |
| NMC622 / Natural Graphite | 10.1 | -2.1 | 4.8 – 6.5 | 1.8 |
| NMC811 / Synthetic Graphite | 10.4 | -3.4 | 6.0 – 8.2 | 2.4 |
| NMC811 / Silicon-Graphite (5 wt% Si) | 18.6 | -3.4 | 11.2 – 15.0 | 4.1 |
Cell vendors often dismiss early face swelling as a normal artifact that stabilizes after formation cycles. Yet field teardowns and lab pressure mapping show that face expansion continues to compound over extended cycling, directly accelerating electrolyte dry-out in high-density core regions.


Gradient
Internal temperature distribution inside large-format prismatic cells follows paths set by material thermal anisotropy and current collector cross-sections. In 280Ah and 304Ah formats, cell dimensions exceed 170 mm in height and 200 mm in width, creating long heat transfer paths from the center out to external cooling interfaces. Heat generated by ohmic resistance, charge transfer kinetics, and entropic changes has to pass through alternating layers of active material, metallic foils, and polymer separators.
Cross-plane thermal conductivity through the laminated stack is low, whereas in-plane conductivity along the aluminum and copper foils is orders of magnitude higher, directing most heat dissipation toward the terminal posts.
Core-to-shell temperature differences widen rapidly under high-rate discharge. Heat generated deep inside the jellyroll cannot easily move perpendicular to the foil planes, raising core temperatures even as active liquid cooling plates keep the outer faces cold. Placing cooling plates only along the bottom of the cell worsens these internal imbalances.
Meanwhile, the top of the electrode stack near the tabs runs hot from combined reaction heat and tab resistance heating. Temperature spreads exceeding 8°C across a single electrode sheet skew current density distribution, accelerating localized degradation.

Anisotropic Conductivity within Laminated Foil Stacks
Thermal conduction through a stacked electrode matrix varies sharply with orientation. Copper current collectors offer thermal conductivity near 390 W/m·K, and aluminum foils deliver about 237 W/m·K. By contrast, microporous polymer separators, porous active coatings, and liquid electrolyte together yield effective cross-plane conductivities of just 0.55 W/m·K to 1.15 W/m·K. Thermal resistance stacks up across thousands of solid-liquid interfaces, forcing core heat to travel along the copper and aluminum foil planes toward the perimeter and terminals rather than straight out through the broad casing faces.
These unequal heat conduction paths produce distinct isothermal contours inside large prismatic housings. Higher temperatures in the core lower local charge-transfer resistance, drawing more current density into those hot central zones. That concentrated current accelerates local electrochemical aging, rapidly consuming active lithium and thickening the solid electrolyte interphase where temperatures peak.
Cooler peripheral areas draw less current, creating uneven state-of-charge profiles across single electrode sheets ~ an internal imbalance that accelerates capacity fade while hiding localized degradation behind module-level voltage readings.
At a continuous 2C discharge in 25°C ambient air, a 280Ah prismatic cell develops a core temperature 14.2°C higher than its outer casing because cross-plane thermal conductivity is so low across the 80-layer separator boundary.

Tab Geometry and Current Density Hotspots
Tab connections at the current collector form major mechanical and thermal bottlenecks in high-capacity prismatic cells. Dozens of cathode and anode foil tabs gather at the top of the stack, joining heavy aluminum and copper terminal blocks via ultrasonic tap welding. Current density spikes where these foils converge.
Because ohmic heat generation at tab-to-terminal junctions grows with the square of operating current, intense hot spots form directly at the top header of the enclosure.
Thermal gradients between the terminals and the bottom casing generate localized thermal stress across the stack structure. Differential expansion forces adjacent electrode layers to shift slightly against each other, straining tab weld roots and separator films. During sustained 2C discharges in 280Ah LFP cells, continuous temperatures above 45°C near terminal welds accelerate local electrolyte breakdown, creating gas pockets that trim the wetted active area on surrounding materials.
What structural modifications to large-format prismatic headers can permanently eliminate localized tab heating without sacrificing energy density?


Deformation
Cyclic thermomechanical forces inside rigid prismatic cans inflict structural damage on internal active layers over extended field service. As graphite anodes expand and contract under tight confinement, stack layers endure constant compressive and shear stresses. Microporous polymer separators ~ usually polyethylene or polypropylene films between 9 µm and 16 µm thick ~ suffer viscoelastic creep and compaction under sustained pressure.
This compaction shrinks pore volume and increases ionic tortuosity, raising cell impedance and driving metallic lithium plating during cold-temperature charging.
Jellyroll micro-buckling is a primary failure mode in prismatic cells exposed to heavy mechanical restraint and thermal cycling. Outer turns of a wound jellyroll or outer layers of a z-folded stack take on sharp bending stresses along tight corner radii. As cyclic swelling forces push outer electrode layers inward against rigid interior cores, the flat sections of the electrode sheets become unstable and buckle into wave-like distortions.
These wrinkled zones suffer immediate active material delamination, severing electrical contact between graphite particles and the copper foil substrate.

Jellyroll Wrinkling and Separator Pore Collapse
Internal electrode distortion develops quietly, leaving no immediate mark on external voltage curves. Once compressive stress crosses 2.0 MPa, the porous matrix of ceramic-coated separators begins to collapse. This pore closure cuts local ionic conductivity, forcing lithium ions sideways toward lower-resistance regions.
Current crowding then develops along the margins of collapsed zones, where localized current density quickly outpaces intercalation kinetics and deposits metallic lithium directly on graphite surfaces during fast charging.
Layer buckling subjects active coating interfaces to severe shear stress. Binder formulations based on polyvinylidene fluoride or styrene-butadiene rubber suffer shear overload under cyclic electrode movement, causing active graphite grains to detach from copper current collectors and leave behind inactive zones. Delamination reduces wetted surface area, driving up local current density across whatever active material remains.
This feedback loop causes irreversible capacity loss and sharp impedance jumps mid-way through cell operating life.

Ultrasonic Tab Weld Fatigue under Cyclic Shear
Internal tab connections experience heavy mechanical fatigue caused by differential thermal expansion between the electrode stack and the outer aluminum housing. Multi-layer foil tabs ~ comprising 30 to 80 individual copper or aluminum foils between 6 µm and 12 µm thick ~ are ultrasonically welded to solid terminal posts. While the internal stack breathes axially and transversely during cycling, the rigid aluminum shell holds its dimensions, subjecting those ultrasonic weld seams to relentless cyclic shear stress.
Micro-cracking starts at high-stress edges around the ultrasonic weld nuggets and works through individual foil layers over thousands of cycles. As individual tabs snap, the surviving foils carry larger shares of the current. The higher current density increases local ohmic heating, driving fatigue cracks across adjacent foils even faster.
Complete tab separation causes an open-circuit failure, or severe internal arcing if loose contact lingers under vibration.

How Does Mechanical Constraint Pressure Alter Plating Thresholds?
Mechanical compression directly controls when metallic lithium plating begins in constrained cells. When external preload squeezes the electrode stack past optimal limits, separator pore compression restricts liquid electrolyte diffusion. Lower ionic transport creates high concentration overpotentials during fast charging, dropping anode potential below 0 V relative to lithium metal and making plating thermodynamically favorable over intercalation.
Plated metallic lithium forms mossy or dendritic deposits at the separator-anode interface, consuming liquid electrolyte and reacting with organic solvents while threatening to pierce compressed separator membranes. Micro-shorts occur when dendrites bridge damaged separators, generating localized heat that degrades surrounding polymer further. Unconstrained test packs develop tab fatigue cracking after 1,200 thermal shock cycles.
| Failure Mechanism | Physical Root Cause | Non-Destructive Diagnostic Signature | Destructive Analysis Finding |
|---|---|---|---|
| Jellyroll Micro-Buckling | Excessive lateral compression during anode expansion | Early high-frequency EIS real impedance growth | Wavy electrode distortion and local active layer detachment |
| Separator Pore Collapse | Continuous mechanical overload above 2.5 MPa | Mid-frequency charge transfer resistance increase | Translucent thinned polymer film with zero porosity |
| Tab Weld Fatigue Fracture | Cyclic shear strain from thermal differential expansion | Erratic DC internal resistance spikes under vibration | Shear crack propagation across ultrasonic weld nuggets |
| Localized Lithium Plating | Ionic tortuosity rise from compressed separator pores | Low-temperature charge profile voltage plateaus | Metallic silver deposit patches on anode surfaces |
Operational protocols in manufacturing facilities should isolate distinct failure modes during teardown audits:
- Active Material Delamination Copper current collector foil detaches from the graphite coating under cyclic interfacial shear during lithiation and delithiation.
- Separator Transverse Creep Polymer separator membranes stretch and thin near outer jellyroll bend radii under continuous pressure, narrowing electrical isolation margins.
- Terminal Weld Micro-Fissuring High-current ultrasonic joints form fatigue cracks due to differential thermal expansion between stack tabs and top cover components.
- Electrolyte Void Formation Expanding gas forces liquid electrolyte out of inner electrode pores into casing corners, triggering dry-out degradation.
Clause 7.4 of UN 38.3 vibration testing misses micro-buckling inside prismatic cans because high ambient field temperatures lower separator yield strength well below the levels tested on room-temperature shakers.
Testing unconstrained prismatic modules on aggressive fast-charge cycles risks internal electrode buckling, triggering sudden micro-short circuits across the lot.


Preload
Managing mechanical stress over the life of prismatic cells demands precise module compression design. Because graphite anodes swell predictably during lithiation, cell thickness grows systematically from fresh out of the factory to end-of-life. Rigid, unyielding module frames with no elastic compliance cause extreme internal pressure build-up: forces past 3.0 MPa can develop by end-of-life, crushing internal separators and driving rapid capacity decay.
On the flip side, assembling cells with too little initial force allows electrode sheets to delaminate and shift under vehicle vibration, accelerating capacity loss through interfacial impedance growth.
Dynamic compression systems place engineered elastomeric foam pads between the broad cell faces inside a module housing. These compressible buffers absorb reversible state-of-charge expansion while accommodating irreversible, long-term thickness growth. Microcellular polyurethane and silicone foams yield flat compression-force-deflection curves, keeping pressure inside a narrow target window across changing compression distances.
For commercial prismatic cells, the target compression window spans 0.2 MPa to 0.6 MPa. Operating in this range suppresses material delamination without crushing separator pores or choking electrolyte diffusion.

Elastomeric Foam Compression Curves and Aging Decay
The choice of inter-cell buffer foam determines long-term mechanical stability in energy storage packs. Foams exhibit complex viscoelastic behavior, relaxing stress under sustained strain and taking a thermal compression set at elevated temperatures. Over years of operation, continuous mechanical load reduces the push-back force from elastomeric pads.
If the foam relaxes faster than the cell swells, contact pressure drops below minimum threshold limits when discharged, allowing internal layers to separate.
A foam’s compression set characteristics under thermal cycling govern its service life. Exposure to temperatures above 50°C under 30 percent strain degrades polymer cross-links, causing permanent loss of thickness. When cells cool during park periods, degraded foam pads fail to hold minimum pressure, opening voids between cells.
Evaluating cell swelling rates across vendor batches verifies manufacturing consistency.

Rigid End Plate Sizing and Structural Deflection Analysis
End plates at the ends of a cell stack must absorb the cumulative swelling forces of all series cells combined. In a 12-cell module, total force on the end plates equals individual cell swell pressure multiplied by broad face surface area. For a 280Ah cell with face dimensions of 173 mm by 200 mm (0.0346 m² area), an internal swell pressure of 1.0 MPa translates to 34.6 kN of linear force against the end plate assembly.
End plate deflection skews internal pressure distribution across neighboring cells. Flexing end plates bow outward at their centers, relieving pressure on central cell zones while concentrating force along perimeter tie-rods. As a result, central cells swell locally and displace electrolyte while outer cells remain over-compressed.
Proper end plate design relies on finite element structural analysis to guarantee maximum center deflection stays below 0.5 mm under peak end-of-life loads.
| Material Formulation | Initial CFD @ 25% Strain (kPa) | Compression Set 70°C/22h (%) | Stress Relaxation 1000h (%) | Thermal Resistance (m²·K/W) |
|---|---|---|---|---|
| Microcellular Polyurethane | 250 – 350 | < 5.0 | 12.5 | 0.045 |
| High-Consistency Silicone Foam | 180 – 280 | < 2.5 | 8.0 | 0.062 |
| Cross-Linked Polyolefin Foam | 400 – 550 | 18.0 | 32.0 | 0.038 |
| Aerogel-Silicone Composite Pad | 300 – 420 | < 3.0 | 6.5 | 0.280 |
Module mechanical integration requires a precise assembly sequence to control preload forces:
- Calculate maximum volumetric expansion across all cells in the module string at 100 percent state of charge and end of life.
- Select inter-cell foam pad thickness and density to achieve a 300 kPa target initial preload pressure at nominal stack dimensions.
- Compress stacked cells and foam pads using a calibrated hydraulic assembly press until tie-rod bolt holes align.
- Torque side retention straps and steel end plate fasteners to specified tension values before releasing hydraulic press load.
- Verify post-assembly module dimensions across three planar axes using automated coordinate measurement equipment.
Rigid module framing without compressible inter-cell buffers drives premature capacity loss through localized over-compression and separator damage during aggressive charging.
Standard automotive pack supply agreements now explicitly require that module end plate center deflection stay below 0.35 mm under a continuous 40 kN end-of-life expansion load, forcing integration teams to upgrade from aluminum to reinforced high-strength steel end plates.


Exposure
Commercial exposure from thermomechanical cell degradation shows up on balance sheets as premature warranty claims, higher scrap rates, and unexpected field failures. Datasheet cycle-life ratings reflect highly artificial laboratory conditions: single cells clamped between flat, liquid-cooled aluminum plates under constant spring pressure in temperature-controlled rooms. Real pack environments subject cells to complex thermal gradients, non-uniform foam degradation, and continuous vehicle shock loads.
The gap between flat-plate lab performance and actual module lifetime represents a massive financial risk for energy storage buyers.
Warranty provisioning calculations have to account for how thermomechanical stress accelerates capacity fade. When cell swelling exceeds what the foam buffers can absorb, internal pressure spikes drive low-temperature lithium plating, triggering early knee-point capacity drops. Modules running under uncontrolled thermal gradients develop cell-to-cell capacity divergence within series strings.
The weakest cell hits the lower voltage cutoff early, curtailing total usable energy and forcing pack replacements long before predicted electrochemical end-of-life.

Landed Cost Impact of Over-Constrained Module Framing
Preventing mechanical degradation takes heavier structural framing, costly elastomeric pads, and tighter manufacturing tolerances ~ all of which drive up initial bill-of-materials costs. High-performance microcellular silicone pads cost five to eight times more than basic polyethylene buffers. Heavy steel end plates and tie-straps add parasitic mass, cutting pack-level gravimetric energy density by 6 to 10 percent.
Over-engineering the mechanical structure inflates the upfront landed cost per kilowatt-hour installed.
Under-specifying mechanical restraint leads to far larger long-term liabilities. Accelerated degradation triggers early warranty claims, field service calls, and reputational damage. Specifying compression limits in supply contracts isolates mechanical degradation risks.
Cost per delivered cycle over equipment operating life is the decisive financial metric. Paying a 4 percent upfront landed cost premium for optimized compression pads and rigid end plates cuts the total cost per delivered cycle by extending operational life from 2,500 to over 5,000 cycles.

Factory Acceptance Tolerance Bounds for Cell Thickness
Accepting cell shipments with uninspected thickness variations undermines mechanical baseline targets during module assembly. Prismatic cells vary slightly in thickness during formation and aging. A manufacturing tolerance of ±0.5 mm on a 70 mm cell looks minor on a single datasheet, but stacking eight cells in series creates a potential stack length variance of ±4.0 mm.
Building fixed-length module frames with cells at the upper thickness limit crushes the foam pads and creates extreme initial preload pressure; building with thin cells results in loose fitting and electrode delamination.
Quality control protocols at incoming inspection require automated digital thickness gauging of every cell under specified contact pressure. Sorting cells into tight dimensional bins before module assembly allows integration lines to match foam pad thickness directly to stack dimensions.
- Dimensional Batch Sorting Audit incoming inspection logs must confirm automated thickness measurements at 30 percent state of charge under 100 kPa uniform plate contact pressure.
- Compression Deflection Certification material batch test certificates for buffer pads must verify that density and force-deflection metrics meet specification bounds within ±5 percent.
- Thermal Expansion Mapping qualification dossiers must contain multi-axis dilatometry data detailing cell thermal expansion coefficients across operating temperatures from -20°C to 60°C.
- End of Life Swell Projections supplier technical files must include irreversible thickness growth projection models validated by at least 2,000 cycles on mechanical test channels.
A sound operational framework for prismatic module integration sets initial assembly preload to the minimum pressure needed to prevent delamination, letting inter-cell foam cushions absorb state-of-charge expansion without exceeding maximum separator yield stress at end of life.